Description
Working Principle & Process Superiority
Plasma Transferred Arc (PTA) welding is a high-energy density thermal surfacing process that utilizes a constricted plasma arc to melt both the metallic substrate surface and specialized hardfacing alloy powder simultaneously. Unlike conventional arc welding or thermal spraying, PTA generates a true metallurgical bond between the coating layer and the substrate, completely eliminating the risk of spallation, delamination, and peeling under severe mechanical impact and thermal cycling.
The constricted transferred arc produces a columnar, concentrated heat input that results in an exceptionally narrow Heat Affected Zone (HAZ) and minimal workpiece thermal distortion. Coupled with our high-precision CNC powder delivery feeder, alloy powders are injected directly into the plasma arc column just above the molten pool, maximizing powder capture efficiency (≥ 92%) and delivering single-pass cladding thicknesses ranging from 0.8 mm to 6.0 mm with pristine surface smoothness.
General Technical Specifications & Parameter Matrix
| Technical Parameter | Specification Standard & Range |
|---|---|
| Input Power Supply | 3-Phase 380V / 415V / 480V ±10%, 50/60 Hz (Configurable to destination country) |
| Main Transferred Arc Current | 30 A – 350 A / 500 A (100% Heavy-Duty Industrial Duty Cycle, IGBT Inverter Controlled) |
| Pilot Arc Current Range | 5 A – 50 A (High-frequency non-contact electronic arc ignition) |
| Base Metal Dilution Rate | 3% – 8% (Adjustable via plasma gas velocity, current density, and travel speed) |
| Powder Deposition Rate | 1.5 kg/h to 10.0 kg/h (Up to 12.0 kg/h with high-power heavy cladding torch) |
| Single Pass Cladding Thickness | 0.8 mm – 6.0 mm (Multi-pass accumulation up to 25 mm+ without delamination) |
| Cladding Bead Width | 3.0 mm – 45.0 mm (Steplessly adjustable via electronic mechanical oscillation unit) |
| Powder Feeder Capacity | Dual Hopper System (5L × 2), precision disc/screw micro-feeding, rate 5–120 g/min, accuracy ±1% |
| Gas Control System | Electronic Mass Flow Controller (MFC) for Plasma Gas (Ar), Shielding Gas (Ar/Ar+H2), and Carrier Gas |
| Cooling System | Integrated High-Flow Refrigeration Chiller (Closed-loop deionized water, cooling capacity ≥ 5.0 kW) |
| HMI & Control Interface | 10.4-inch / 15-inch Siemens / Delta Color Touchscreen with 100+ program recipe storage & USB backup |
Advanced Subsystems & Engineering Highlights
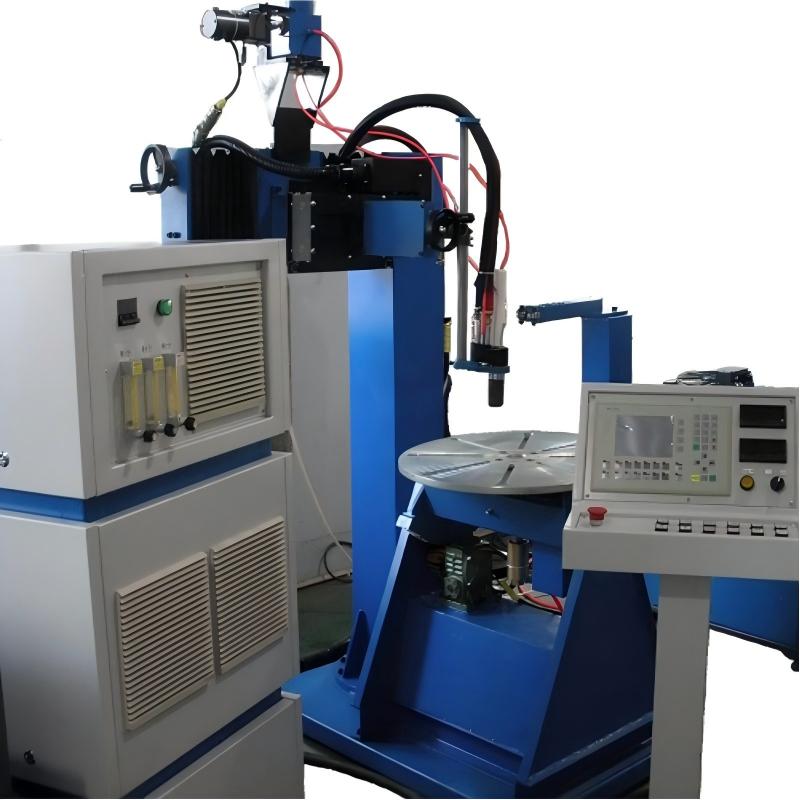
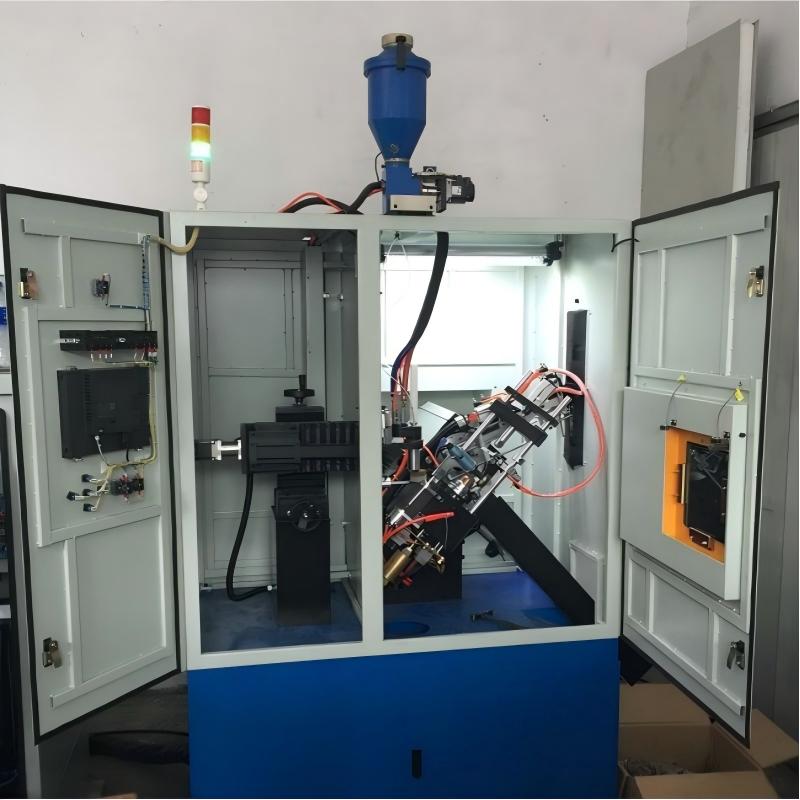
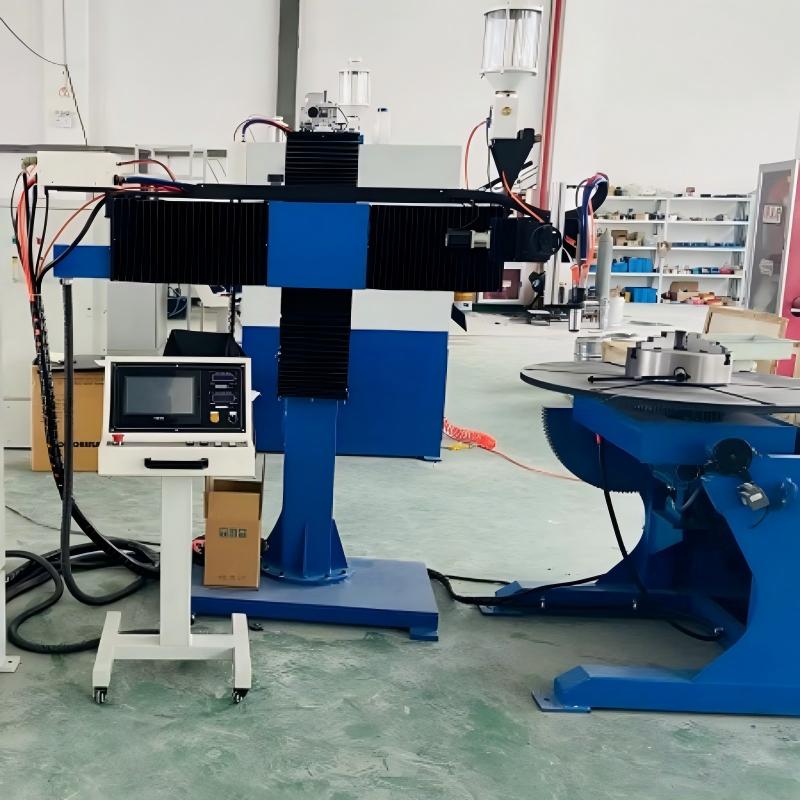
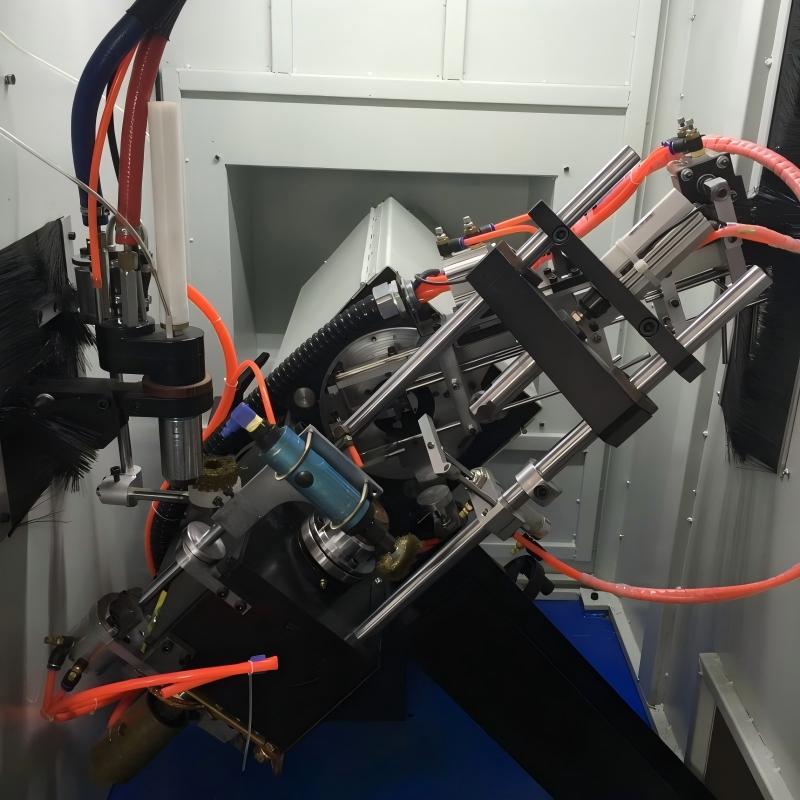
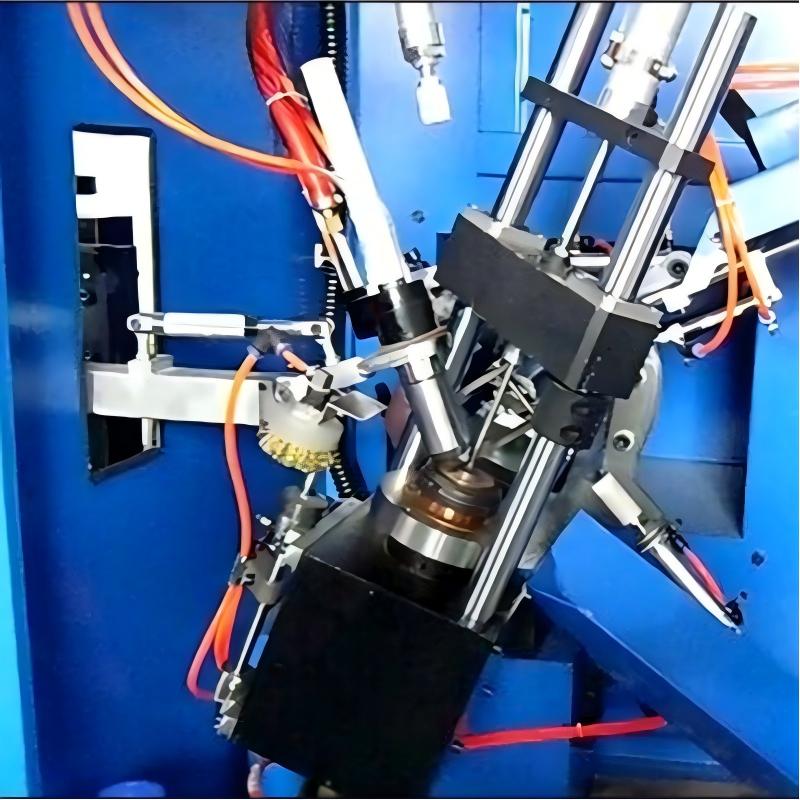
Our PTA welding machines integrate industrial-grade modules engineered for 24/7 continuous operation in rigorous manufacturing environments:
•1. Advanced IGBT Inverter Power Source: Delivers microsecond-level dynamic constant-current response. Features dual independent control for the pilot arc (non-transferred) and main transferred arc, guaranteeing instant arc ignition and rock-solid arc stability even during wide torch-to-workpiece distance variations.
•2. Dual-Chamber Precision CNC Powder Feeder: Equipped with variable-speed disc metering and internal heated dehumidification hoppers to prevent powder clumping. Supports seamless gradient alloy feeding (e.g., buffering layer transition to ultra-hard top layer) with digital feedback monitoring.
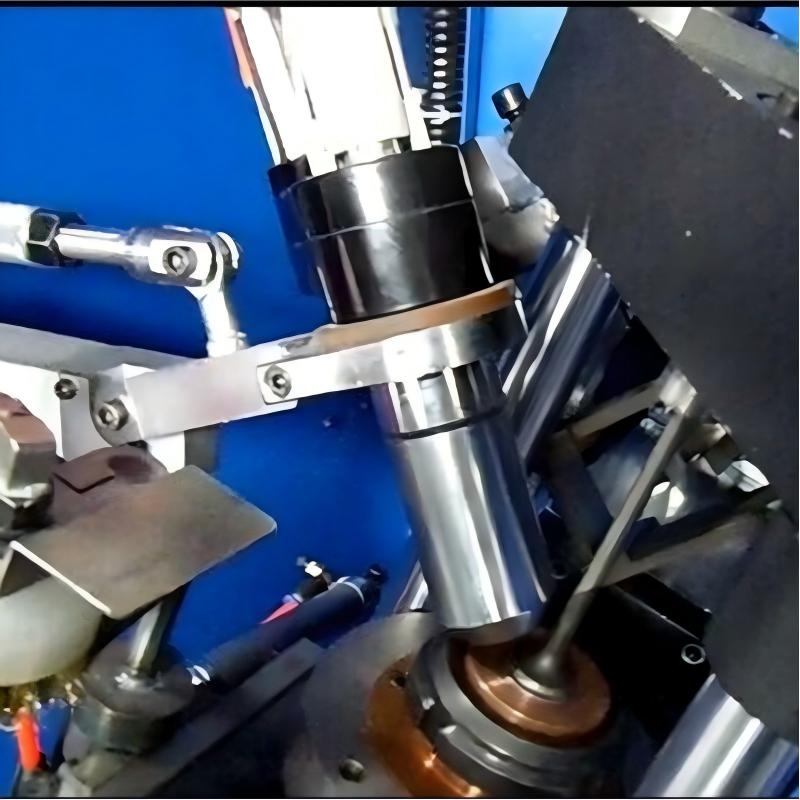
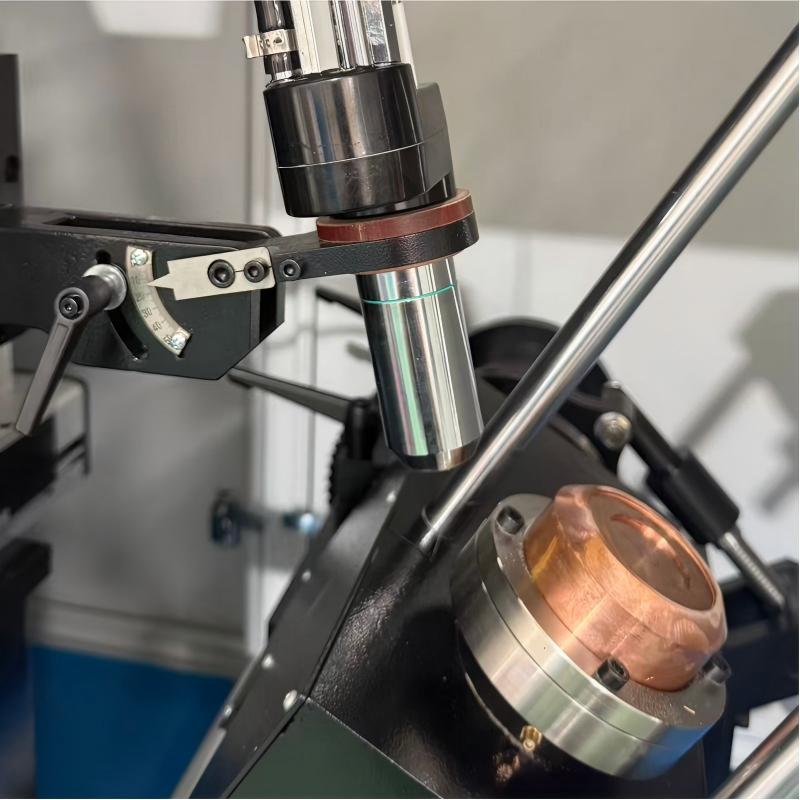
•3. Heavy-Duty Multi-Channel Water-Cooled Plasma Torch: Precision CNC-machined copper alloy nozzle with concentric powder injection channels. Optimized internal cooling jackets ensure long tungsten electrode and nozzle service life even under continuous 350A+ heavy-duty operation.
•4. Real-Time Arc Voltage Control (AVC) & Seam Tracking: High-speed closed-loop height sensor continuously samples arc voltage and adjusts the Z-axis in real time (response 2,200 HV) for severe gouging and drilling wear.
•Iron-Base & Tool Steel Alloys: High-Chromium Cast Iron (Fe-Cr-C, 58–64 HRC), Martensitic Stainless Steels (410/420), and H13 hot-work tool steel powders for cost-effective remanufacturing of heavy rolls and dies.
Process Comparison: PTA vs. Traditional Hardfacing Technologies
A direct technical comparison highlighting why global manufacturers are transitioning to automated PTA surfacing:
| Comparison Feature | PTA Welding | Laser Cladding | TIG / GTAW Wire | Thermal Spray & Fuse |
| Base Metal Dilution | 3% – 8% (Minimal) | 2% – 5% (Ultra-low) | 12% – 20% (High) | 0% (Spray) / 5%–10% (Fuse) |
| Bonding Mechanism | 100% True Metallurgical Bond | 100% True Metallurgical Bond | 100% True Metallurgical Bond | Mechanical lock (Spray) / Fused bond |
| Deposition Rate | High (2.0 – 10.0 kg/h) | Moderate (1.0 – 4.5 kg/h) | Low (0.8 – 1.8 kg/h) | Moderate to High (2.0–6.0 kg/h) |
| Capital Equipment Cost | Moderate (Fast ROI within 6–12 mos) | Very High (3x – 5x of PTA) | Low | Moderate (Requires 2-step furnace/torch) |
| Powder / Material Versatility | Extremely Broad (Stellite, Ni, WC, Fe) | Broad (Requires high optical absorption) | Limited to drawn welding wire alloys | Self-fluxing alloys only |
| Operational Maintenance Cost | Low (Standard gas/nozzle consumables) | High (Optics, laser diodes, fiber cables) | Low (High manual labor cost) | High (Oxy-fuel gases & furnace energy) |
Key Application Industries & Components
| Industry Sector | Critical Wear / Corrosion Challenges | Typical PTA Cladded Components |
|---|---|---|
| Plastics & Polymer Compounding | Extreme abrasive wear from 30%–60% glass fiber, mineral fillers, and corrosive corrosive halogen-free flame retardants. | Twin-screw extruder flight tops, single-screw barrier flights, mixing head tips, feed zone feed screws. |
| Industrial Valves & Pumps | High-pressure steam wire drawing, cavitation erosion, and galling on metal-to-metal sealing surfaces. | Gate valve wedges, seat rings, globe valve plugs, safety relief valve discs, slurry pump impellers. |
| Oil & Gas / Downhole Drilling | Severe abrasive gouging from rock formations, sour gas (H2S), and high-velocity abrasive drilling mud. | Drill bit stabilizers, reamer blades, MWD tool joints, mud motor rotors, subsea choke valve trims. |
| Power Generation & Energy | High-temperature erosion from pulverized coal fly ash, molten salt corrosion, and thermal fatigue cycling. | Boiler waterwall tube overlays, coal pulverizer roller tires, steam turbine valve stems, sootblower nozzles. |
| Mining, Cement & Steel Mills | Heavy impact combined with severe mineral sliding abrasion and high-temperature oxidation. | Crusher hammer tips, clinker grinding rolls, continuous casting pinch rolls, hot shear knives, excavating teeth. |
Reviews
There are no reviews yet.