Description
Product Overview
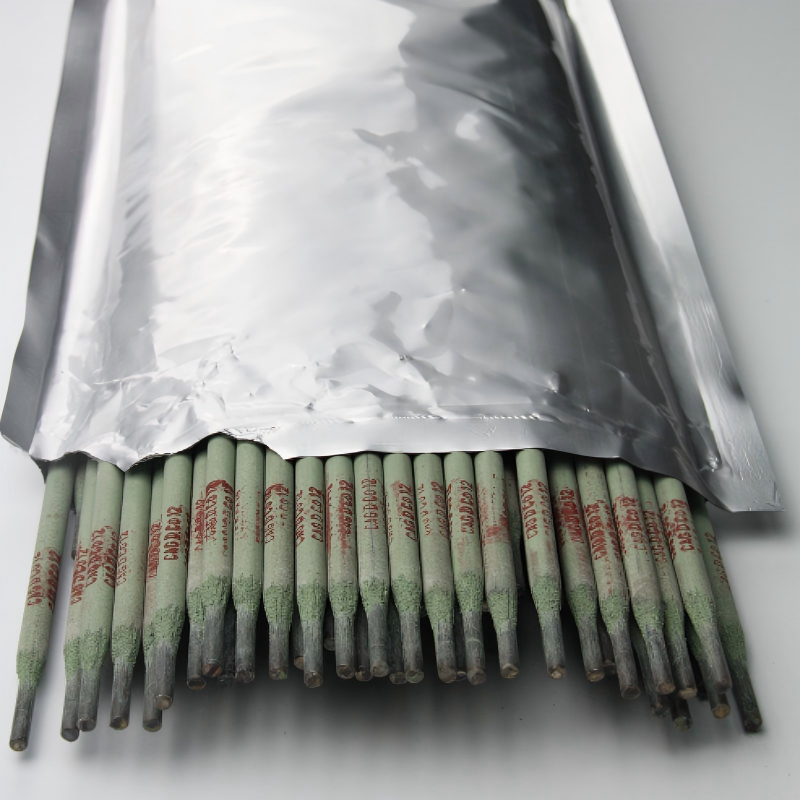
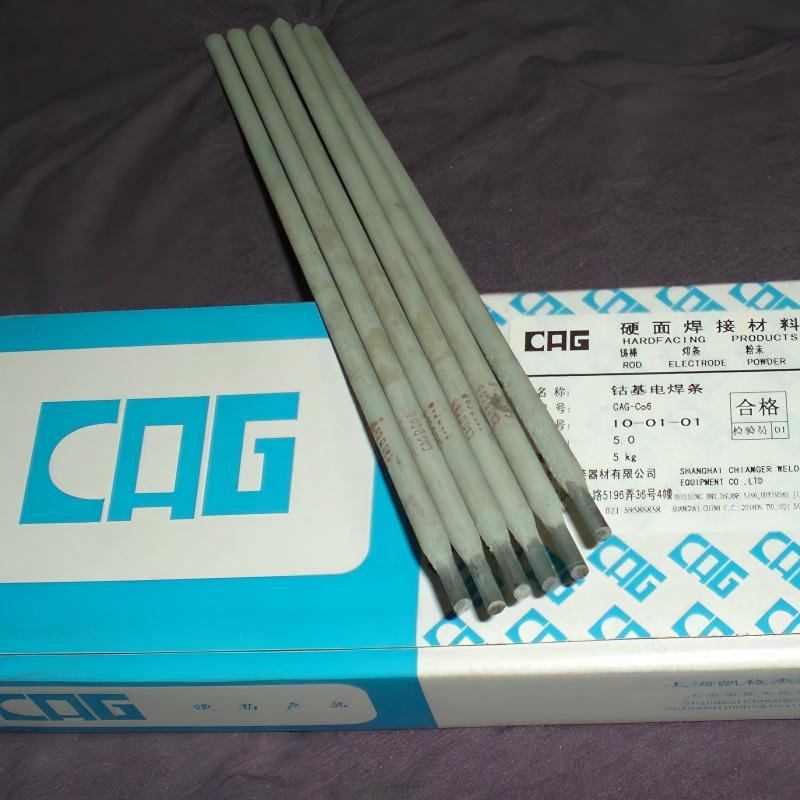
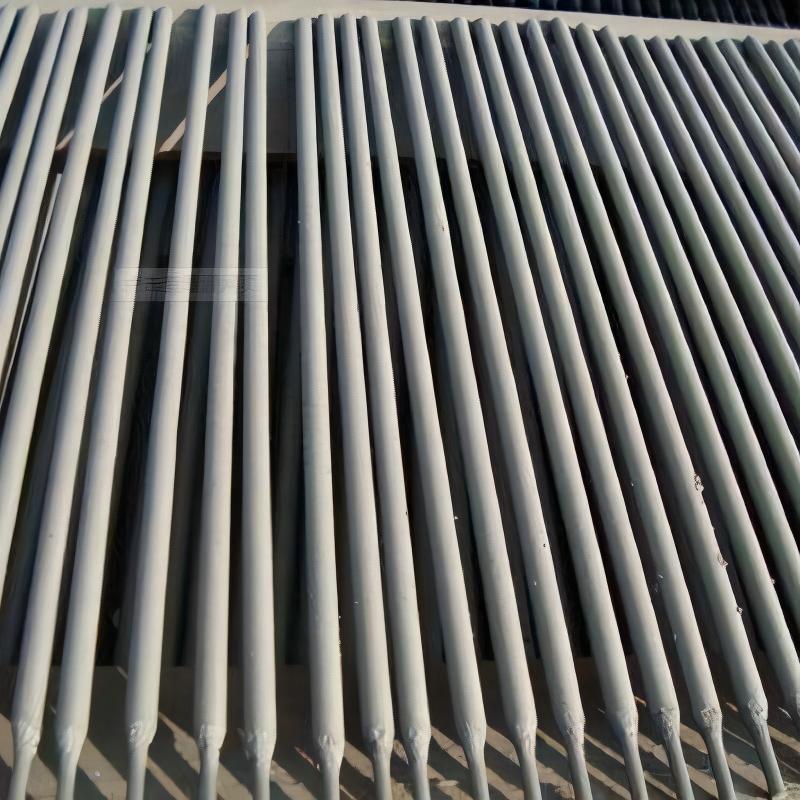
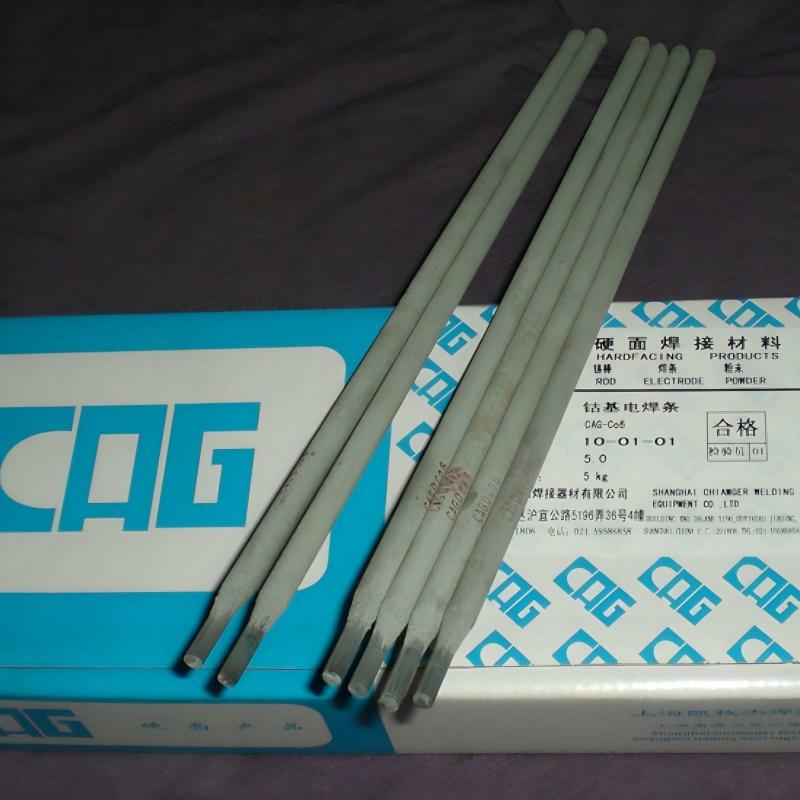
Our Cobalt-Base Welding Electrodes (Shielded Metal Arc Welding / Stick Electrodes) feature high-purity cast cobalt alloy cores with specially formulated low-hydrogen rutile/basic coatings. Designed for manual hardfacing and in-situ repairs, these electrodes deposit a cobalt-chromium-tungsten solid solution matrix heavily reinforced with dispersion-hardened eutectic carbides.
When automated cladding is impractical or on-site field repair is required, our cobalt-base electrodes provide flawless weldability on AC and DC+ currents, exceptional wetting characteristics, minimal substrate dilution, and crack-free deposits that restore worn components to OEM or higher-than-OEM specifications.
Core Technical & Operational Advantages
1.Outstanding Operating Characteristics & Arc Control: Smooth, concentrated arc with minimal spatter loss, stable re-ignition, and easy-to-remove slag—even in out-of-position field repair.
2.High-Temperature Hardness Retention (Red Hardness): Maintains exceptional mechanical integrity, compressive strength, and wear resistance up to 650°C – 800°C, resisting annealing softening under thermal cycling.
3.Exceptional Galling & Friction Resistance: Low friction coefficient in metal-to-metal sliding contact prevents seizing, scuffing, and adhesive galling without fluid lubrication.
4.Superior Cavitation & High-Pressure Fluid Erosion Resistance: Withstands aggressive high-velocity steam throttling, cavitation erosion, and oxidizing chemical environments.
5.Low Dilution & Excellent Base Metal Fusion: Controlled penetration prevents excessive iron pickup from carbon or alloy steel substrates, ensuring the full hardfacing property is achieved already in the 1st or 2nd layer.
| Cobalt—Base Electrodes | ||||||||||||
| Trademark | Nominal Chemical Composition(wt%) | HRC | Application | Reference Standard | ||||||||
| C | Cr | Si | W | Ni | Fe | Mn | Mo | Co | ||||
| CAG-D Co1 | 2.10 | 30.00 | 1.00 | 14.00 | ≤ 3.00 | ≤ 5.00 | ≤ 2.00 | ≤ 1.00 | Bal | 48-54 | Valve seat inserts, bearing, cutter edge, etc. | ECoCr-C Stellite 1 |
| CAG-D Co6 | 1.00 | 30.00 | 1.00 | 4.60 | ≤ 3.00 | ≤ 5.00 | ≤ 2.00 | ≤ 1.00 | Bal | 38-44 | High temperature valves, saw teeth, turbine blade | ECoCr-A Stellite 6 |
| CAG-D Co12 | 1.40 | 30.00 | 1.00 | 9.00 | ≤ 3.00 | ≤ 5.00 | ≤ 2.00 | ≤ 1.00 | Bal | 44-48 | High temperature pressure valves, saw teeth, screw flights, etc. | ECoCr-B Stellite 12 |
| CAG-D Co21 | 0.20 | 28.00 | 1.00 | — | ≤ 3.00 | ≤ 5.00 | ≤ 2.00 | 5.50 | Bal | 20-40 cold hard |
Valve seat insert, brass casting die, etc. | ECoCr-E Stellite 21 |
| CAG-D Co25 | 0.15 | 20.00 | 1.00 | 14.00 | 10.00 | ≤ 5.00 | ≤ 2.00 | ≤ 1.00 | Bal | cold hard | High temperature and corrosion-resistant valve sealing surface, pressure casting dies | Stellite 25 |
| *Note: Deloro Stellite is a registered trademark. | ||||||||||||
Standard Dimensions & Welding Parameter Guidelines
| Diameter | Standard Length | Current Type | Recommended Current | Weld Position |
|---|---|---|---|---|
| Ø 2.5 mm (3/32″) | 300 mm / 350 mm | DC+ (DCEP) / AC | 60 – 90 A | Flat, Horizontal |
| Ø 3.2 mm (1/8″) | 350 mm | DC+ (DCEP) / AC | 90 – 125 A | Flat, Horizontal |
| Ø 4.0 mm (5/32″) | 350 mm | DC+ (DCEP) / AC | 120 – 160 A | Flat, Horizontal |
| Ø 5.0 mm (3/16″) | 350 mm / 400 mm | DC+ (DCEP) / AC | 150 – 200 A | Flat |
Recommended Welding & Preheating Procedure:
1. Surface Preparation: Grind base metal thoroughly to remove rust, grease, fatigue cracks, or old work-hardened layers.
2. Preheat Temperature:
• Carbon & Low-Alloy Steels: 250°C – 350°C (480°F – 660°F).
• Martensitic/Ferritic Stainless Steels: 350°C – 450°C (660°F – 840°F).
3. Interpass Temperature: Maintain interpass temperature equal to or slightly above preheat temperature.
4. Post-Weld Cooling: Slow cooling in insulated lime, dry vermiculite, or controlled furnace to prevent thermal stress cracking.
Target Industries & Typical Engineering Components
Industrial Valves & Petrochemical: Gate valve wedges, globe valve discs, high-pressure steam valve seats, and slurry control trim.
Power Generation & Nuclear Energy: Turbine governor valves, main steam stop valves, boiler blowdown valves, and pulverizer components.
Iron & Steel Mills: Hot shear blades, entry/exit guide rollers, tong bits, blooming mill guides, and coiler mandrels.
Pulp, Paper & Recycling: Chipper knives, defibrator bars, plastic granulator cutter edges, and decanter centrifuge wear shoes.
Mining & Heavy Earthmoving: Excavator bucket teeth, drill bit heads, crusher wear liners, and slurry pump wear sleeves.
Packaging & Quality Compliance
Packaging:
• Inner Pack: 5.0 kg / hermetically sealed tin can or vacuum-sealed moisture-resistant plastic box.
• Outer Pack: 20 kg / master carton (4 × 5 kg), palletized and stretch-wrapped for overseas maritime/air shipment.
Quality Assurance Documents:
• Material Test Certificate (MTC) per heat batch (Chemical Composition & Deposited Hardness).
• AWS A5.21 / A5.13 Compliance Certification.
• Detailed Welding Procedure Specification (WPS) & Parameter Guidelines.
Reviews
There are no reviews yet.