Description
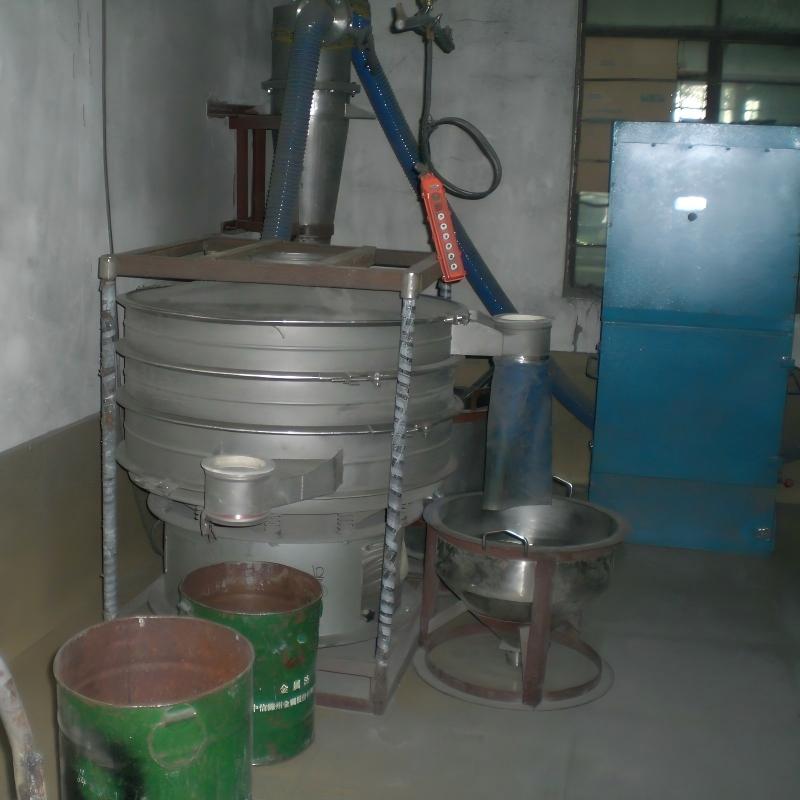
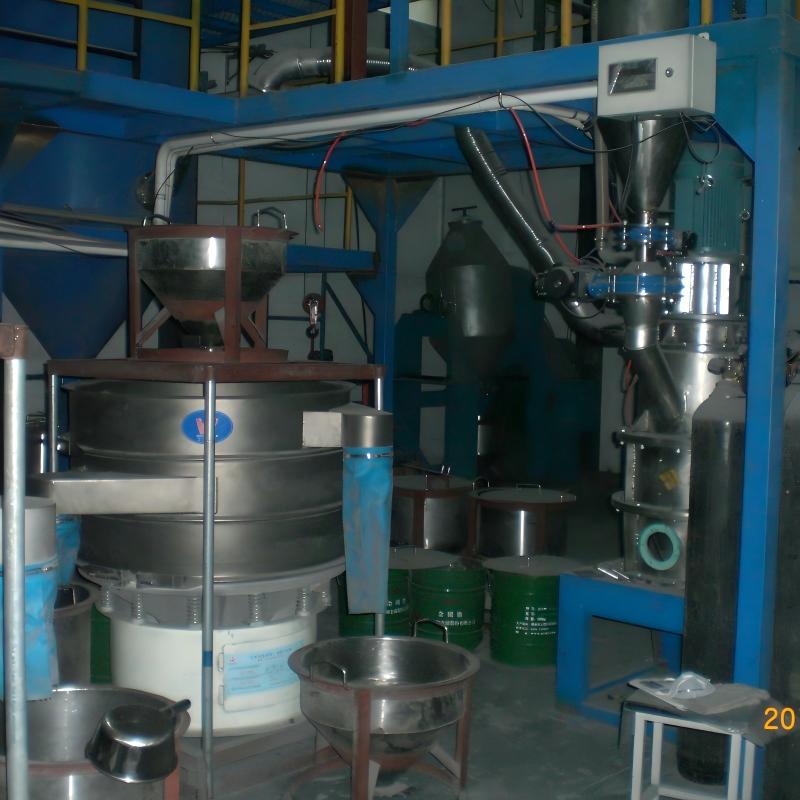
VIGA Gas Atomization Technology
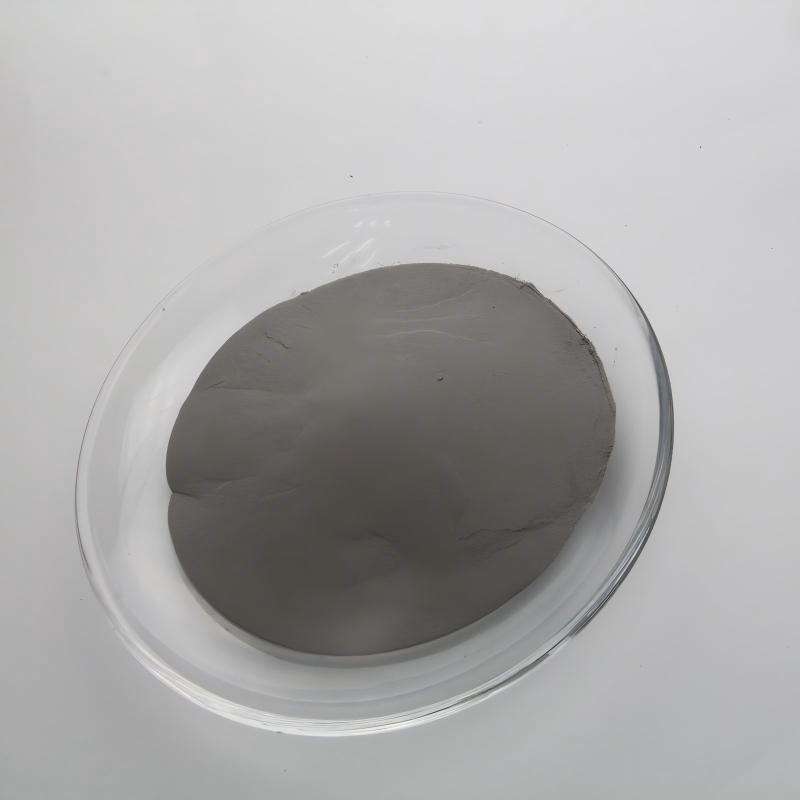
nickel-base welding powders are manufactured using advanced inert gas atomization (VIGA / EIGA) under ultra-high vacuum and high-purity argon shielding. Liquid metal streams are atomized by supersonic gas nozzles, yielding perfectly spherical powders with smooth surfaces, minimal satellite attachment, and tightly controlled particle size distribution.
The alloy matrix consists of a ductile nickel-solid-solution austenite phase heavily reinforced with in-situ precipitated ultra-hard chromium borides (CrB, Cr5B3, hardness > 1800 HV) and chromium carbides (Cr7C3, Cr23C6). Boron (B) and Silicon (Si) act as powerful self-fluxing agents: Silicon deoxidizes the molten pool and promotes wettability, while Boron depresses the melting point and forms self-healing intermetallic phases during deposition.
| Nickel—Base Alloy Powder | ||||||||||||||
| Trademark | Nominal Chemical Composition(wt%) | HRC | Application | Reference Standard | ||||||||||
| C | Cr | Si | W | Ni | Fe | Mn | Mo | Co/Cu | B | P | ||||
| CAG-Ni20A | ≤ 0.10 | 4.50 | 2.00 | — | Bal | — | — | — | — | 0.70 | — | 18-22 | glass molds, various forming dies, etc | — |
| CAG-Ni22A | 0.20 | 1.00 | 2.80 | — | Bal | ≤ 1.00 | ≤ 0.10 | — | — | 1.40 | — | 20-24 | glass molds, various forming dies, etc | — |
| CAG-Ni28A | ≤ 0.10 | 3.00 | — | — | Bal | — | — | — | — | 1.00 | — | 26-30 | glass molds, various forming dies, etc | — |
| CAG-Ni30A | 0.15 | 3.00 | 2.60 | — | Bal | ≤ 5.0 | ≤ 0.10 | — | — | 1.40 | — | 24-28 | gear teeth, slide rail, etc | — |
| CAG-Ni35A | 0.20 | 4.00 | 3.20 | — | Bal | ≤ 5.0 | ≤ 0.10 | — | — | 1.60 | — | 32-37 | valve seat, etc | — |
| CAG-Ni37A | 0.15 | 4.50 | 2.60 | — | Bal | — | — | — | — | 1.20 | — | 35-40 | glass molds, plunger, various forming dies, etc | — |
| CAG-Ni40A | 0.30 | 7.50 | 3.60 | — | Bal | ≤ 5.0 | ≤ 0.10 | ≤ 0.10 | — | 1.70 | — | 36-44 | screw feeder, die inserts, etc | — |
| CAG-Ni50A | 0.40 | 12.00 | 3.80 | — | Bal | ≤ 5.0 | ≤ 0.10 | ≤ 0.10 | — | 2.20 | — | 46-54 | pump shaft, pulp knives, screw rod, etc | — |
| CAG-Ni60A | 0.70 | 15.00 | 4.00 | — | Bal | ≤ 5.0 | ≤ 0.10 | ≤ 0.10 | — | 3.20 | — | 57-62 | plunger extrusion press, pump impeller, etc | — |
| CAG-Ni6325A | 0.70 | 16.00 | 4.00 | — | Bal | ≤ 5.0 | ≤ 0.10 | 3.00 | Cu: 3.00 | 3.40 | — | 57-62 | corrosion resistance pump shaft, bearing sleeve, etc | — |
| CAG-Ni25 | 0.20 | 1.00 | 3.50 | — | Bal | 8.00 | — | — | — | 1.50 | — | 22-27 | glass molds, various forming dies, etc | — |
| CAG-Ni35 | 0.30 | 10.00 | 3.50 | — | Bal | 10.00 | — | — | — | 2.00 | — | 32-37 | glass molds, various forming dies, etc | — |
| CAG-Ni45 | 0.50 | 12.00 | 3.80 | — | Bal | 10.00 | — | — | — | 2.40 | — | 42-48 | exhaust valve, plunger, etc | — |
| CAG-Ni55 | 0.80 | 15.00 | 4.00 | — | Bal | 14.00 | — | 3.00 | Cu: 3.00 | 3.00 | — | 52-58 | plunger, drawing roller, etc | — |
| CAG-Ni60 | 0.90 | 15.00 | 3.80 | — | Bal | 15.00 | — | — | — | 3.50 | — | 58-62 | plunger, easily worn parts | — |
| CAG-Ni62 | 1.00 | 16.00 | 3.80 | 10.00 | Bal | 14.00 | — | — | — | 3.80 | — | 59-64 | Shovel teeth, paper break wheel, easily worn parts, etc | — |
Particle Size & Process Compatibility
| Welding / Thermal Process | Particle Size Range (µm) | Mesh Equivalent | Powder Feed Characteristics |
| Laser Cladding | 45 – 105 µm (or 53 – 150 µm) |
-140 / +325 Mesh (-100 / +270 Mesh) |
Zero satellite, rapid in-flight melting, dense metallurgical track with <1% porosity. |
| Plasma Transferred Arc (PTA) | 45 – 150 µm (or 75 – 180 µm) |
-100 / +325 Mesh (-80 / +200 Mesh) |
Stable powder stream, high deposition efficiency (>90%), minimal torch nozzle wear. |
| High-Velocity Oxygen-Fuel (HVOF) | 15 – 45 µm (or 15 – 53 µm) |
-325 / +500 Mesh | Ultra-fine spherical particles, supersonic acceleration, low porosity (<0.5%) coatings. |
| Flame Spray & Fuse (OAW Spray) | 38 – 106 µm (or 45 – 125 µm) |
-140 / +400 Mesh (-120 / +325 Mesh) |
Self-fluxing action during torch reflow, smooth puddle wetting, defect-free seal. |
| Atmospheric Plasma Spray (APS) | 20 – 53 µm | -270 / +500 Mesh | High melting efficiency in high-temp plasma jet, uniform wear-resistant barrier. |
Key Engineering Advantages
【01 / Flow & Sphericity】
1. Superior Particle Sphericity & Powder Flowability
VIGA atomization ensures sphericity index ≥ 92% with smooth particle contours. Hall Flow Rate measured at < 15.0 s/50g (ASTM B213), eliminating powder bridging, nozzle clogging, and pulsed feeding during multi-axis automated laser cladding or high-speed PTA runs.
【02 / Clean Chemistry】
2. Ultra-Low Oxygen Content & Pure Metallurgical Track
Strict inert gas vacuum processing maintains oxygen content below 150 ppm (LECO TC500 analyzed). Low oxygen minimizes oxide stringers and microporosity, maximizing bonding strength and crack resistance in demanding cyclic thermal and mechanical fatigue applications.
【03 / High Utilization & ROI】
3. High Deposition Efficiency & Minimal Dilution
Tight PSD prevents under-melted coarse particles or evaporated ultra-fines. Deposition powder utilization efficiency exceeds 85%-92% in laser cladding and 90%-95% in PTA, dramatically lowering material consumption and total overlay cost per square meter.
【04 / Extreme Protection】
4. Extreme Corrosion & Severe Wear Resistance
Chromium borides (CrB) and carbides (Cr7C3) combined with solid-solution nickel matrix deliver outstanding resistance against low-angle particle erosion, high-temperature cavitation, chloride pitting, and H2S/CO2 sulfide stress cracking.
Target Industrial Applications
| Industry Sector | Critical Components | Recommended Grade & Technology |
| Oil & Gas / Drilling Equipment | Drilling tool stabilizers, downhole motor rotors, drill bit claddings, MWD/LWD housings. | Ni60 + 50% WC Composite (PTA / Laser): Resists high-stress gouging abrasion in deep well drilling. |
| Valve & Flow Control | Ball valve spheres, valve seats, control chokes, high-pressure steam valve trims. | Ni60 / Alloy 625 (Laser Cladding / PTA): Zero-leakage sealing, cavitation erosion & acid corrosion resistance. |
| Power & Boiler Engineering | Boiler waterwall tubes, superheater tube shields, sootblower lances, turbine blade roots. | NiCr-B-Si / Alloy 625 (High-Speed Laser Cladding): High-temperature sulfur & chlorine hot-corrosion protection. |
| Polymer & Plastic Compounding | Twin-screw kneading blocks, barrel feed sections, pelletizer rotor blades, die plates. | Ni60 / Ni55 (Laser Cladding / PTA): Resists severe glass-fiber wear and halogen flame-retardant acid attack. |
| Glass & Metal Forming Tooling | Glass container plungers, neck rings, blow molds, hot extrusion guide rollers. | Ni35 / Ni45 (Flame Spray & Fuse / PTA): Thermal fatigue resistance, smooth glass release, easy mirror polishing. |
Quality Assurance & Test Certification
• Particle Size Distribution (PSD) Analysis: 100% verified using Malvern Mastersizer 3000 Laser Diffraction Particle Size Analyzer .
• Powder Flowability & Apparent Density: Tested strictly in accordance with ASTM B213 (Hall Flowmeter) and ASTM B212 / B527 (Apparent / Tap Density).
• Chemical Purity & Gas Analysis: Optical Emission Spectrometry (OES) / ICP-OES for elemental makeup; LECO Oxygen/Nitrogen/Hydrogen analyzers for gas purity.
• SEM Morphology & Cross-Sectional Analysis: Scanning Electron Microscopy (SEM) verification to ensure satellite-free and pore-free internal particle density.
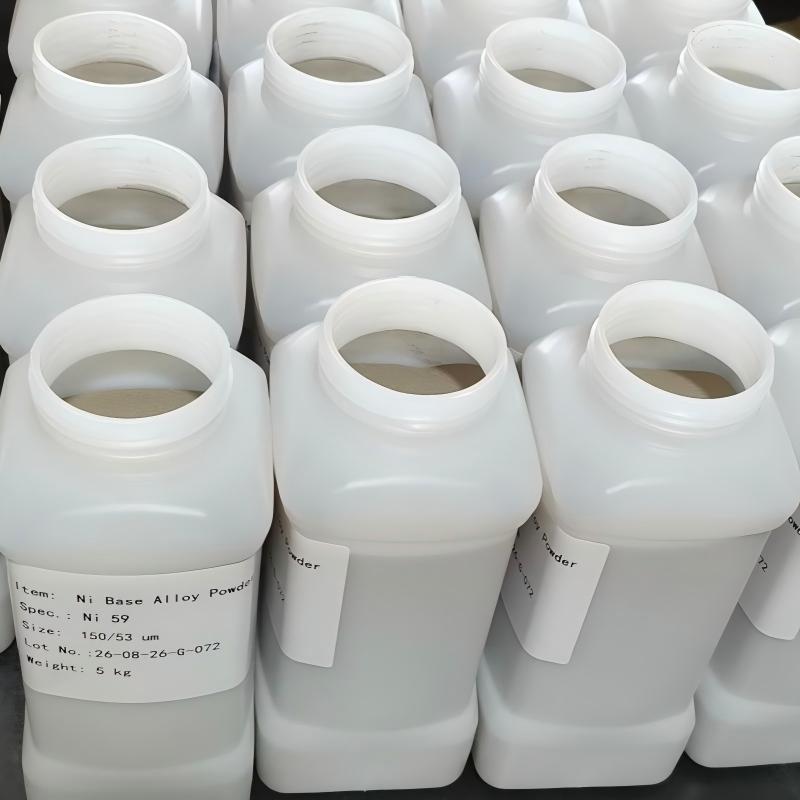
• Packaging Standards: 5 kg / 10 kg / 25 kg sealed aluminum-foil vacuum bags in high-density polyethylene (HDPE) drums, nitrogen-flushed for long shelf-life.
Reviews
There are no reviews yet.