Description
| Cobalt—Base Bare Rods | ||||||||||||
| Trademark | Nominal Chemical Composition(wt%) | HRC | Application | Reference Standard | ||||||||
| C | Cr | Si | W | Ni | Fe | Mn | Mo | Co | ||||
| CAG-Co1 | 2.45 | 30.00 | 1.00 | 13.00 | ≤ 3.00 | ≤ 3.00 | ≤ 1.00 | ≤ 1.00 | Bal | 50-58 | Valve seat inserts, bearing, cutter edge, rotary ring, etc. | AWS A5.21 ERCoCr-C Stellite 1 |
| CAG-Co3 | 2.40 | 30.50 | 1.00 | 13.00 | ≤ 3.00 | ≤ 3.00 | ≤ 1.00 | ≤ 1.00 | Bal | 50-56 | Valve seat inserts, steel mill guide roll, wearing panel of cracker blade, etc. | AWS A5.21 ERCoCr-C Stellite 3 |
| CAG-Co4 | 1.00 | 31.00 | 1.00 | 14.00 | ≤ 3.00 | ≤ 1.00 | ≤ 0.50 | ≤ 0.50 | Bal | 45-50 | Hot extrusion die, dry battery industry | Stellite 4 |
| CAG-Co6 | 1.20 | 29.00 | 1.00 | 4.50 | ≤ 3.00 | ≤ 3.00 | ≤ 1.00 | ≤ 1.00 | Bal | 40-46 | Engine valve, high temperature valves, turbine blade, etc. | AWS A5.21 ERCoCr-A Stellite 6 |
| CAG-Co12 | 1.40 | 30.00 | 1.30 | 8.50 | ≤ 3.00 | ≤ 3.00 | ≤ 1.00 | ≤ 1.00 | Bal | 44-50 | High temperature, pressure valves, saw teeth, screw flights, etc. | AWS A5.21 ERCoCr-B Stellite 12 |
| GAG-Co20 | 1.40 | 32.00 | 1.20 | 17.00 | ≤ 3.00 | ≤ 3.00 | ≤ 0.50 | ≤ 1.00 | Bal | 54-59 | Bearing sleeve, wear plate | Stellite 20 |
| CAG-Co21 | 0.25 | 27.00 | 1.00 | 0.20 | ≤ 3.00 | ≤ 2.00 | ≤ 1.00 | ≤ 5.50 | Bal | 20 | Fluid valve, brass casting die, valve seat, etc. | AWS A5.21 ERCoCr-E Stellite 21 |
| CAG-Co25 | 0.05 | 20.00 | 1.00 | 15.00 | 10.00 | ≤ 2.00 | ≤ 1.50 | ≤ 1.00 | Bal | cold hard | High temperature and corrosion-resistant valve sealing surface, pressure casting dies, etc. | Stellite 25 |
| CAG-Co31 | 0.50 | 26.00 | 1.00 | 7.50 | 10.00 | ≤ 3.00 | ≤ 1.00 | ≤ 1.00 | Bal | 30-35 | Extrusion die, steam turbine blade, etc. | Stellite 31 |
| CAG-CoF | 1.80 | 26.00 | 1.00 | 12.00 | 22.00 | ≤ 1.50 | ≤ 0.50 | ≤ 1.00 | Bal | 40-45 | Engine inlet and exhaust valve | AWS A5.21 ERCoCr-F Stellite F |
| CAG-Co190 | 3.20 | 26.00 | 1.00 | 14.00 | ≤ 1.00 | ≤ 3.00 | ≤ 1.00 | ≤ 1.00 | Bal | ≥ 54 | Petroleum drill bit | AWS A5.21 ERCoCr-G Stellite 190 |
| CAG-CoT-400 | 0.08 | 8.50 | 2.60 | — | 1.50 | ≤ 1.50 | ≤ 1.00 | ≤ 28.00 | Bal | 50-60 | Wedge gate valves at elevated temperature, corrosive environment, plastic extrusion liners | Tribaloy T-400 |
| CAG-CoT-800 | 0.08 | 18.00 | 3.40 | — | ≤ 1.50 | ≤ 1.50 | ≤ 1.00 | ≤ 28.00 | Bal | 52-58 | Wedge gate valves at elevated temperature, corrosive environment, plastic extrusion liners | Tribaloy T-800 |
| *Note: Deloro Stellite is a registered trademark. | ||||||||||||
Specifications and Packaging Standards (Supply Capabilities Packaging)
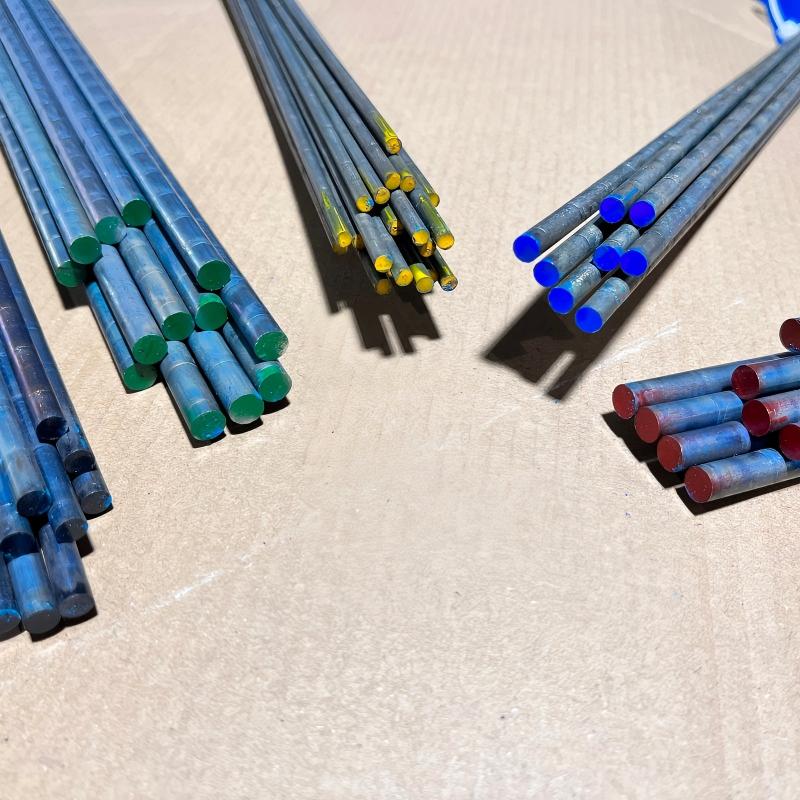
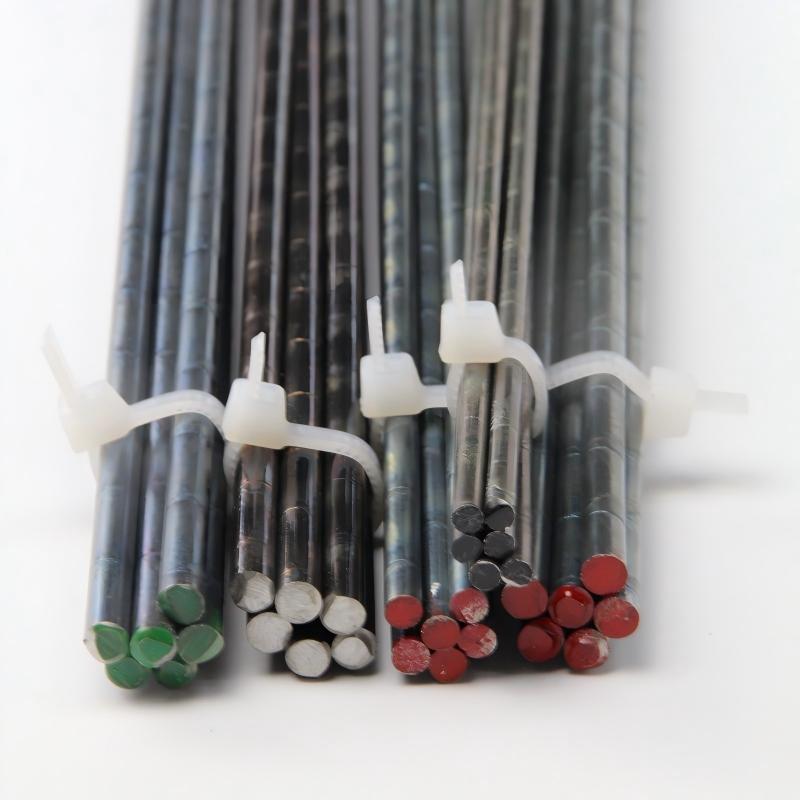
Standard diameters: Ø 2.5 mm, Ø 3.2 mm, Ø 4.0 mm, Ø 5.0 mm, Ø 6.4 mm (tolerances strictly controlled)
Standard length: 1000 mm (39″), custom short bars of 500 mm and 350 mm are also available.
Surface Finish: Pickled/Ground Clean, smooth surface free of oxide scale and grease.
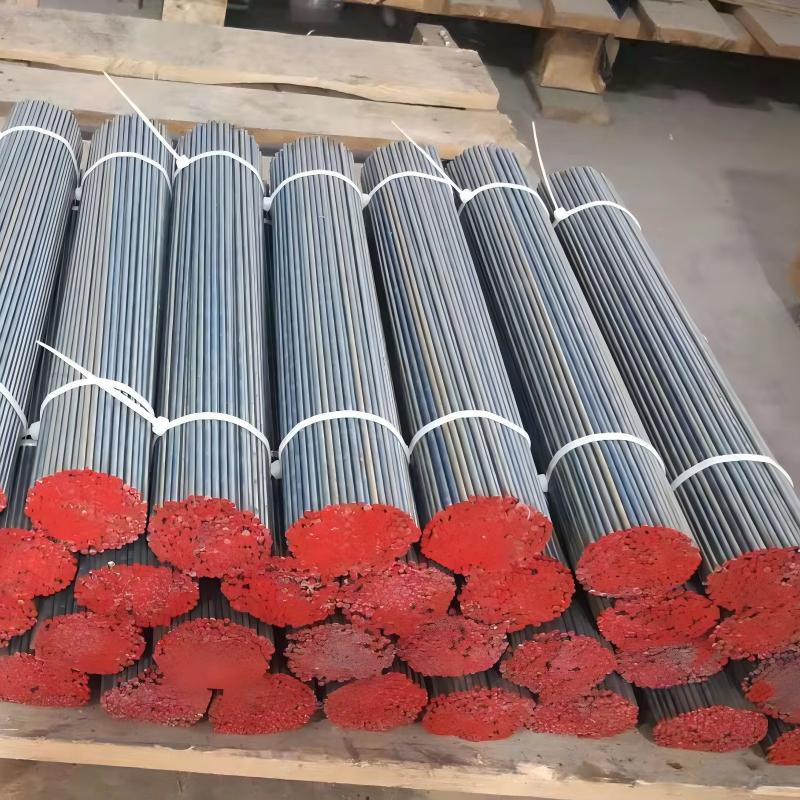
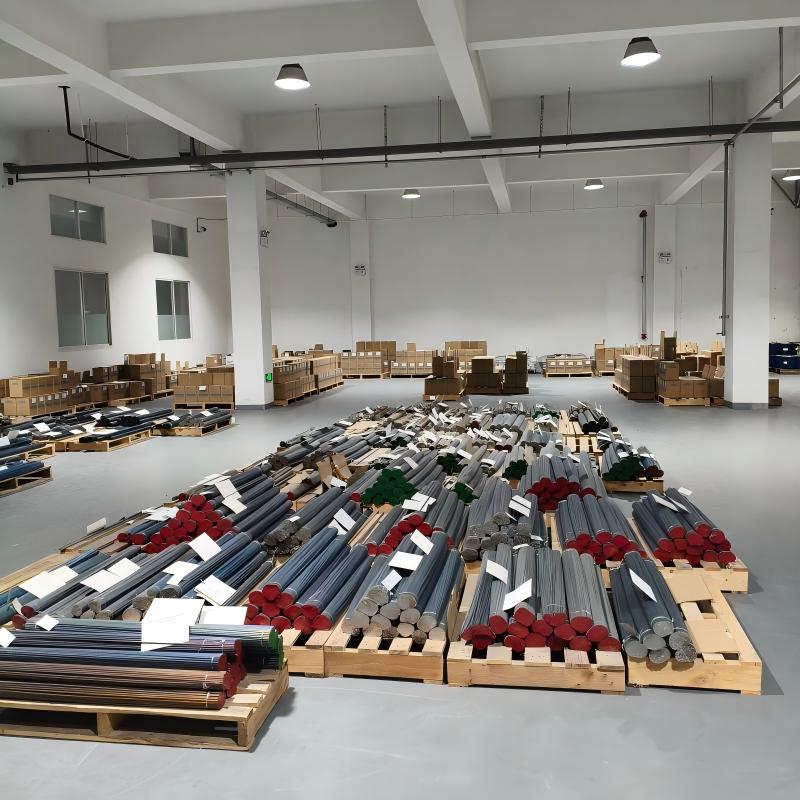
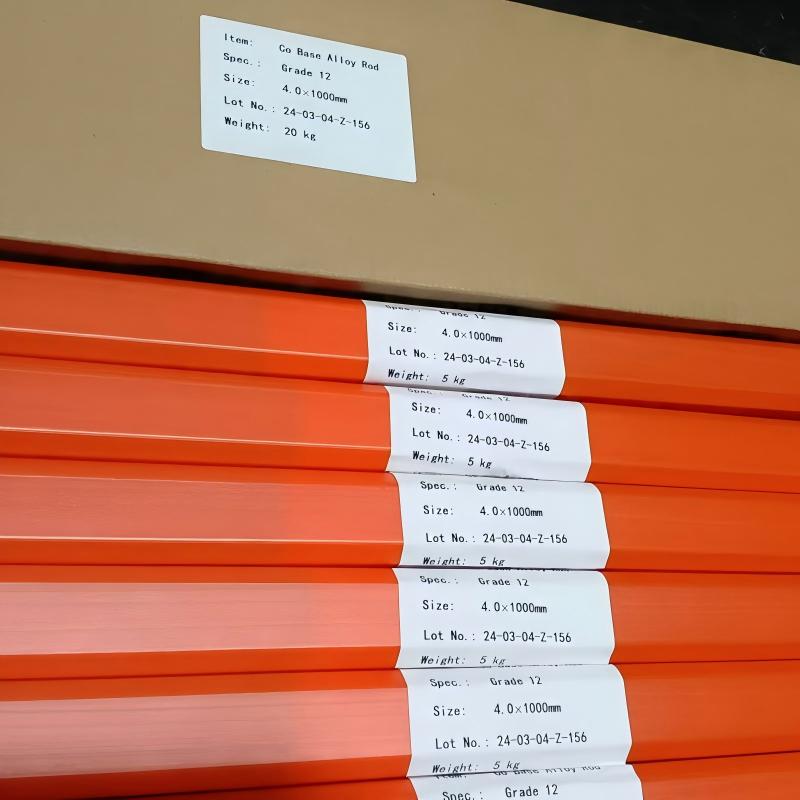
Standard Packaging: 5 kg / 10 kg sealed moisture-proof plastic tube packaging, outer high-strength cardboard box / export-grade fumigation-free wooden box
Recommended Welding Parameters
TIG (Tranquil Arc Welding) Process Recommendations (GTAW Guidelines):
Polarity: DCEN (Direct Current Positive)
Protective gas: High-purity argon (Argon ≥ 99.99%), recommended flow rate 8–14 L/min
Preheating temperature: 250°C – 450°C is recommended depending on the base material to prevent thermal stress cracking of the weld overlay.
Post-weld slow cooling: It is recommended to place the welded material in an insulated furnace or asbestos-insulated area to slowly cool to room temperature.
Oxy-acetylene welding guidelines:
A carburizing flame is used to strictly control the melting depth of the base material in order to maintain an extremely low dilution rate.
Quality Assurance Testing
Strict raw material control: We use virgin, high-purity metal raw materials and reject inferior recycled waste.
Batch composition traceability: Direct-reading spectroscopy (OES) composition testing is performed on each batch to ensure precise and controllable carbides and trace elements.
Internal flaw detection and flowability test: Samples of each batch of welding wire are tested on weld overlay test plates to inspect the weld metal by X-ray flaw detection (RT), penetrant testing (PT) and hardness of the weld overlay.
Factory documents: Material Quality Certificate (MTC), Welding Procedure Qualification Guide (WPS supplementary reference) and TDS are provided with the order.
Reviews
There are no reviews yet.